For a contractor, 95% compaction is not a roller setting or a fixed number of passes. It is a measurable relationship between the dry density achieved in the field and the maximum dry density established for the material under the specified laboratory procedure.
Reaching that target consistently depends on controlling the entire process: material condition, moisture, lift thickness, equipment selection, machine operation, site access, testing, and documentation
What Does 95% Compaction Actually Mean?
Before field compaction begins, a representative soil sample is normally tested in a laboratory using a specified compaction procedure. The test establishes two important reference values:
- Maximum dry density (MDD)
- Optimum moisture content (OMC)
The maximum dry density represents the reference density that the material can achieve under the energy level and procedure of that laboratory test. The optimum moisture content indicates the approximate moisture condition at which that density is most efficiently achieved.
Suppose the laboratory establishes a maximum dry density of 120 lb/ft³. If the project specification requires 95% relative compaction, the field material needs a dry density of approximately 114 lb/ft³ or greater.
| Laboratory / Field Value | Example |
| Maximum dry density | 120 lb/ft³ |
| Required compaction | 95% |
| Minimum field dry density | 114 lb/ft³ |
| Actual tested dry density | 116 lb/ft³ |
| Approximate relative compaction | 96.7% |
| Result | Pass |
The important point is that 95% is a comparison with the laboratory reference, not a direct measurement of how “hard” the ground feels.
This is also why two soils compacted beside each other can have different acceptable field densities. Their laboratory maximum dry densities may be different.
Why Projects Specify 95% Compaction
Loose fill contains soil particles, water, and void spaces. When a structure, pavement, slab, retaining wall, or pipeline is placed over poorly compacted material, future loading can rearrange the soil structure and reduce the void space.
That movement appears at the surface as settlement.
Proper compaction creates a denser and more stable soil structure before the permanent construction load is applied. Its benefits vary by soil type and application, including improved:
- Bearing performance
- Resistance to settlement
- Pavement support
- Stability of engineered fill
- Consistency between different areas of the site
- Performance around foundations and structures
- Resistance to deformation under repeated traffic
A 95% requirement therefore provides a measurable acceptance criterion. Instead of relying on statements such as “we rolled it six times” or “the ground feels hard,” the project has a testable target.
95% Compaction Does Not Mean Every Project Uses the Same Standard
This is one of the details contractors should check before starting work.
A specification stating only “compact to 95%” is incomplete without identifying the laboratory reference method or applicable project standard. Different laboratory procedures apply different compaction energies and can establish different maximum dry densities for the same material.
As a result, 95% of one laboratory reference is not necessarily equivalent to 95% of another.
The contractor should confirm the project requirements before mobilizing the compaction operation.
| Item to Confirm | Why It Matters |
| Required percentage | Establishes the acceptance target |
| Laboratory test method | Defines the reference maximum dry density |
| Soil/material type | Influences equipment and moisture control |
| Required lift thickness | Affects whether the full layer can be compacted |
| Moisture requirements | Influences achievable density |
| Test frequency | Determines inspection and production planning |
| Testing locations | Prevents untested weak areas |
| Acceptance procedure | Clarifies what happens after a failed test |
On many projects, different areas can also have different requirements. General landscaping fill may not have the same specification as structural fill beneath a slab or pavement.
Always work from the project specification rather than assuming 95% applies universally.
How Moisture Content Affects Maximum Dry Density
Contractors often focus on density and treat moisture as a secondary issue. In practice, moisture is one of the biggest reasons compaction operations either become efficient or frustrating.
Imagine trying to compact completely dry granular or fine material. Particles may resist rearranging because friction between them is relatively high. Adding an appropriate amount of water can help particles move into a denser arrangement.
But more water does not continuously improve compaction.
Once the material becomes excessively wet, water occupies more of the available void space and the soil may begin pumping, rutting, weaving, or sticking to the compaction equipment. Additional rolling may accomplish very little.
This creates three practical conditions.
Material Too Dry
Typical field signs include loose surfaces, dust, poor cohesion, and density results that improve slowly despite repeated passes.
The practical response may be to add water, mix it thoroughly through the lift, allow moisture to equalize, and compact again.
Material Near the Suitable Moisture Range
The soil generally responds efficiently to compactive effort. Density increases predictably and fewer unnecessary passes are required.
This is where contractors want the operation to remain.
Material Too Wet
The surface may look firm initially but move under the roller. Wheel rutting, pumping, displacement, or material sticking to drums can appear.
Continuing to add compaction passes is rarely the best solution. The material may need aeration, drying, remixing, or replacement depending on site conditions and specifications.
Why More Roller Passes Do Not Always Produce Higher Density
One of the most expensive mistakes in earthwork is treating failed compaction as a simple lack of roller passes.
If four passes do not achieve the target, the instinct is often to make eight. When eight fail, the crew tries twelve.
Sometimes additional passes are exactly what is needed. Sometimes they only burn fuel and time.
Compaction performance can be limited by several variables:
- Incorrect moisture content
- Lift thickness exceeding the machine’s effective compaction depth
- Compactor type poorly matched to the material
- Insufficient machine weight or compactive energy
- Incorrect travel speed
- Material segregation or inconsistent soil
- Soft or unstable underlying layers
- Poorly mixed moisture
- Restricted access around structures
- A laboratory reference that does not represent the material currently being placed
A failed density test should therefore be treated as process information, not simply as an instruction to keep rolling.
Lift Thickness Is Critical
A roller primarily influences material within a certain effective depth. If the loose lift is too thick, the upper portion may become dense while the bottom remains insufficiently compacted.
This can create a deceptive surface. The ground looks good, equipment travels over it easily, and the upper layer feels hard. Yet testing at the required depth may identify inadequate density.
Consider a contractor trying to place 400 mm of fill in one lift when the equipment and material combination can effectively compact only a much thinner layer. Increasing the number of surface passes may not deliver enough energy to the bottom of that lift.
The better production strategy is usually:
Place → level → condition moisture → compact → test → approve → place next lift.
Thinner lifts require more placement cycles, but excessively thick lifts can create even greater delays through failed tests, rework, excavation, and recompaction.
The correct lift thickness should be established from project requirements, soil characteristics, equipment capability, and field trials.
Match the Compactor to the Material
There is no single “best” soil compactor.
A large machine that works extremely well on one material can be inefficient on another because different soils respond to different forms of compactive effort.
| General Material | Common Compaction Approach | Main Consideration |
| Sand and gravel | Vibratory compaction | Particle rearrangement responds well to vibration |
| Granular base | Vibratory roller | Density and surface control |
| Cohesive soil | Padfoot/sheepsfoot-type compaction | Kneading action through the lift |
| Mixed soil | Application-dependent | Moisture and gradation become important |
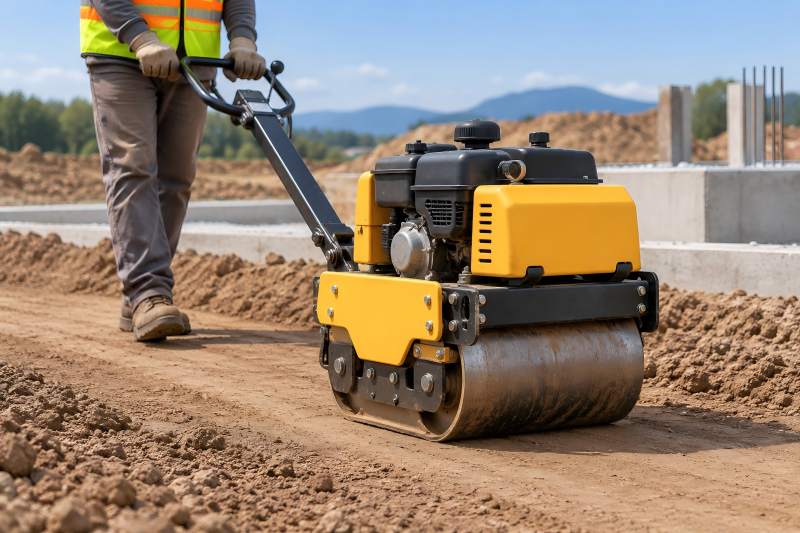
| Narrow trenches | Trench roller or plate equipment | Access and effective depth |
| Around structures | Smaller controlled equipment | Avoid damage while achieving uniform density |
Equipment selection should consider more than operating weight. Vibration characteristics, drum configuration, contact pressure, amplitude, frequency, travel speed, and lift depth all influence the result.
How Is 95% Compaction Verified in the Field?
The field test determines the actual dry density of the compacted material. That result is compared with the appropriate laboratory maximum dry density.
Depending on the project, field density may be evaluated using methods such as nuclear density testing, sand cone testing, or other approved procedures.
The basic verification sequence is straightforward:
- Obtain representative material information and establish the laboratory reference.
- Place the fill at the approved lift thickness.
- Adjust and distribute moisture as required.
- Compact the lift using the selected equipment and operating pattern.
- Test field density and moisture.
- Compare field dry density with the applicable laboratory maximum.
- Accept the lift or perform corrective work.
- Document the result before covering the tested layer.
The percentage alone is not enough. The contractor should also pay attention to where the test was performed and which material reference was used.
A Passing Test Does Not Automatically Mean the Entire Area Is Good
This is an important practical limitation of density testing.
A test represents a particular location. A large fill area may contain hundreds or thousands of cubic meters of material, while only a limited number of locations are physically tested.
For example, a passing test in the center of a roadway does not automatically prove that compaction beside a manhole, around a pipe, against a retaining wall, or along the edge of the fill is equally good.
Weak zones commonly develop where normal equipment cannot operate effectively.
Contractors should pay special attention to:
- Utility trench edges
- Areas beside foundations
- Corners
- Around manholes and structures
- Pipe haunches and bedding zones
- Fill transitions
- Areas inaccessible to large rollers
- Locations where equipment turns frequently
- Material placed during changing weather conditions
Good quality control therefore combines testing with a repeatable construction process.
What Should You Do When a 95% Compaction Test Fails?
A failed test does not always require removing the entire lift.
First determine why the density is low.
| Field Condition | Likely Issue | Possible Corrective Direction |
| Dry and dusty | Moisture too low | Add and uniformly mix water |
| Soft and pumping | Excess moisture or weak support | Dry, aerate, stabilize, or investigate underlying layer |
| Firm surface, low deeper density | Lift may be too thick | Reduce lift thickness and recompact |
| Density improves with each pass | Insufficient compactive effort | Add controlled passes |
| Little improvement after many passes | Moisture/equipment/material problem | Stop rolling and diagnose |
| Failures only near structures | Access/equipment issue | Use suitable smaller compaction equipment |
| Results vary significantly | Inconsistent material | Check segregation and laboratory reference |
The goal is to correct the cause, not just pass. The goal is to correct the process producing the low density.
That distinction can save substantial time on large earthwork projects.
Establish a Test Strip Before Full Production
For significant earthwork, a short trial section can be extremely valuable.
Instead of immediately placing thousands of cubic meters of material, use a representative area to determine an efficient combination of:
- Loose lift thickness
- Moisture condition
- Compactor type
- Machine settings
- Travel speed
- Number of passes
- Rolling pattern
After compaction, verify density at several locations.
If the target is achieved consistently, the successful procedure becomes a practical starting point for production.
For example, a crew may discover that six passes at an appropriate moisture condition consistently achieve the specification. Running ten passes everywhere would then consume fuel, machine hours, and labor without meaningful benefit.
The opposite can also happen. A trial may show that the planned lift is too thick, allowing the contractor to change the method before large quantities are placed.
Watch the Material, Not Just the Roller
Earthwork conditions change throughout a project.
Material delivered on Monday may not behave exactly like material delivered two weeks later. A borrow area can contain different soil layers. Rain can change moisture dramatically. Hot weather can dry the surface while deeper material remains wet.
A compaction procedure should therefore be repeatable but not blind.
If density results suddenly change, check whether something else changed first:
- Did the source material change?
- Has the gradation changed?
- Did it rain?
- Is the material drying faster?
- Is the lift thicker?
- Has roller speed increased?
- Is the compactor operating correctly?
- Is the underlying layer unstable?
This process-oriented approach is more useful than assuming the equipment is always the problem.
Keep Better Compaction Records
For contractors, density records are more than inspection paperwork. They can become production data.
A useful compaction record can include the area or station, elevation, lift number, material source, laboratory reference, moisture result, field dry density, required percentage, achieved percentage, equipment used, number of passes, test location, date, and corrective action if required.
Over time, these records reveal patterns.
You may discover that one borrow material consistently requires more moisture conditioning, one area repeatedly fails because of drainage, or one combination of lift thickness and roller settings delivers particularly stable results.
That information can improve estimating and planning on future projects.